
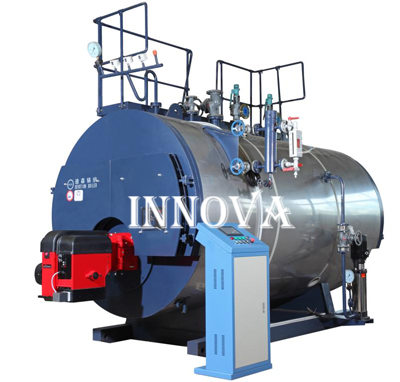
Innovacorp India is a premier manufacturer of advanced Boiler Chemicals in Bhopal, delivering specially formulated solutions that empower modern thermal operations. Our product range is engineered to support scale inhibition, internal conditioning, and significant fuel efficiency improvement for the Bhopal industrial sector. By integrating cutting-edge chemical science with sustainable practices, we help plants in Bhopal achieve superior productivity and enhanced boiler life.
Today’s high-pressure systems face intense challenges, including heat transfer loss. Our specialized Boiler Chemical solutions in Bhopal provide precise, science-backed interventions to prevent scale, ensuring every system reaches its maximum operational potential in the local Bhopal water conditions.
Industrial boiler systems in Bhopal face constant chemical challenges from feedwater impurities. Our Boiler Chemicals in Bhopal are engineered to condition feedwater, stabilize pH, and control mineral deposits, ensuring optimum thermal efficiency and safety. We provide solutions for both high-pressure and low-pressure systems, tailored to the specific water chemistry of the Bhopal region.
Innovacorp provides field-tested, high-performance boiler solutions specifically for the Bhopal market. Our products are compatible with automated dosing systems and are backed by expert technical support to optimize your Boiler Water Treatment Program in Bhopal.
Conclusion:
Effective Boiler Water Treatment in Bhopal is an investment in safety and
profitability. By
integrating Innovacorp’s smart chemistry, Bhopal industries can achieve higher
thermal efficiency and lower
operational costs. Empower your boiler in Bhopal with Innovacorp’s expert chemical
solutions.
© 2026 Innovacorp India Pvt Ltd. All Rights Reserved. Managed & Developed by Innova Corporate India