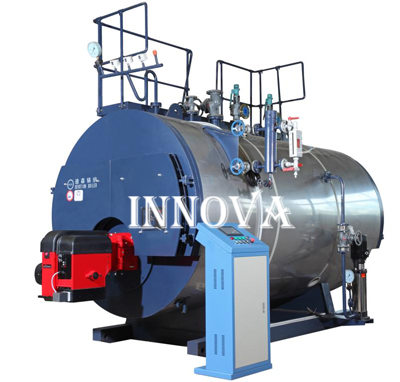
Manufacturers, Exporters, Suppliers of Boiler Chemicals in Haryana

Advanced Boiler Water Treatment Chemicals in Haryana - Innovacorp India

High-Performance Boiler Water Treatment Chemicals in Haryana

Innovacorp India is a leading manufacturer of Boiler Chemicals in Haryana, supporting modern thermal operations. Our product range is engineered for scale inhibition and fuel efficiency for the Haryana industrial sector, helping plants achieve superior productivity and enhanced boiler life.

Optimizing Thermal Efficiency in Haryana Industrial Hubs

High-efficiency steam systems require precise chemical balance. Our specialized Boiler Chemical solutions in Haryana prevent scale and corrosion, ensuring systems reach their maximum operational potential.

Technical Overview: Comprehensive Boiler Conditioning in Haryana

Industrial boiler systems in Haryana face constant chemical challenges from feedwater impurities. Our Boiler Chemicals in Haryana are engineered to condition feedwater, stabilize pH, and control mineral deposits, ensuring optimum thermal efficiency and safety. We provide solutions for both high-pressure and low-pressure systems, tailored to the specific water chemistry of the Haryana region.

Key Functions of Our Boiler Treatment Solutions

  • Scale Inhibitors & Antiscalants: Advanced polymers that prevent calcium and silica deposits on heat transfer surfaces for Haryana industrial units.
  • Oxygen Scavengers: High-speed formulations that eliminate dissolved oxygen to prevent pitting corrosion.
  • Alkalinity Builders & pH Boosters: Precise pH control to protect the boiler metal and feed lines from acidic attack in Haryana plants.
  • Sludge Conditioners & Dispersants: Keeps suspended solids fluid, ensuring easy removal during routine blowdown.
  • Condensate Treatment: Protects steam and condensate return lines from carbonic acid corrosion.

Strategic Benefits for Industrial Plants in Haryana

  • Significant Fuel Savings: Ensures maximum heat transfer, directly reducing energy costs for Haryana refineries.
  • Extended Equipment Life: Robust protection against corrosion reduces the frequency of retubing in Haryana boilers.
  • Steam Purity: Prevents carryover and foaming, ensuring dry steam for sensitive processes.
  • Reduced Downtime: Minimizes unscheduled shutdowns in Haryana Sugar Refineries and Cogeneration Plants.

Application Areas in Haryana

  • Sugar Industry Boilers: High-capacity systems requiring precise chemical balance.
  • Power & Cogeneration: High-pressure boilers where water purity is non-negotiable for Haryana power units.
  • Process Industries: Textiles, Chemical plants, and Food & Beverage manufacturing in Haryana.
  • Auxiliary Systems: Feedwater tanks, deaerators, and condensate return units.

Why Choose Innovacorp India in Haryana?

Innovacorp provides field-tested, high-performance boiler solutions specifically for the Haryana market. Our products are compatible with automated dosing systems and are backed by expert technical support to optimize your Boiler Water Treatment Program in Haryana.

Conclusion:
Effective Boiler Water Treatment in Haryana is an investment in safety and profitability. By integrating Innovacorp’s smart chemistry, Haryana industries can achieve higher thermal efficiency and lower operational costs. Empower your boiler in Haryana with Innovacorp’s expert chemical solutions.

Our Products

Chat on WhatsApp